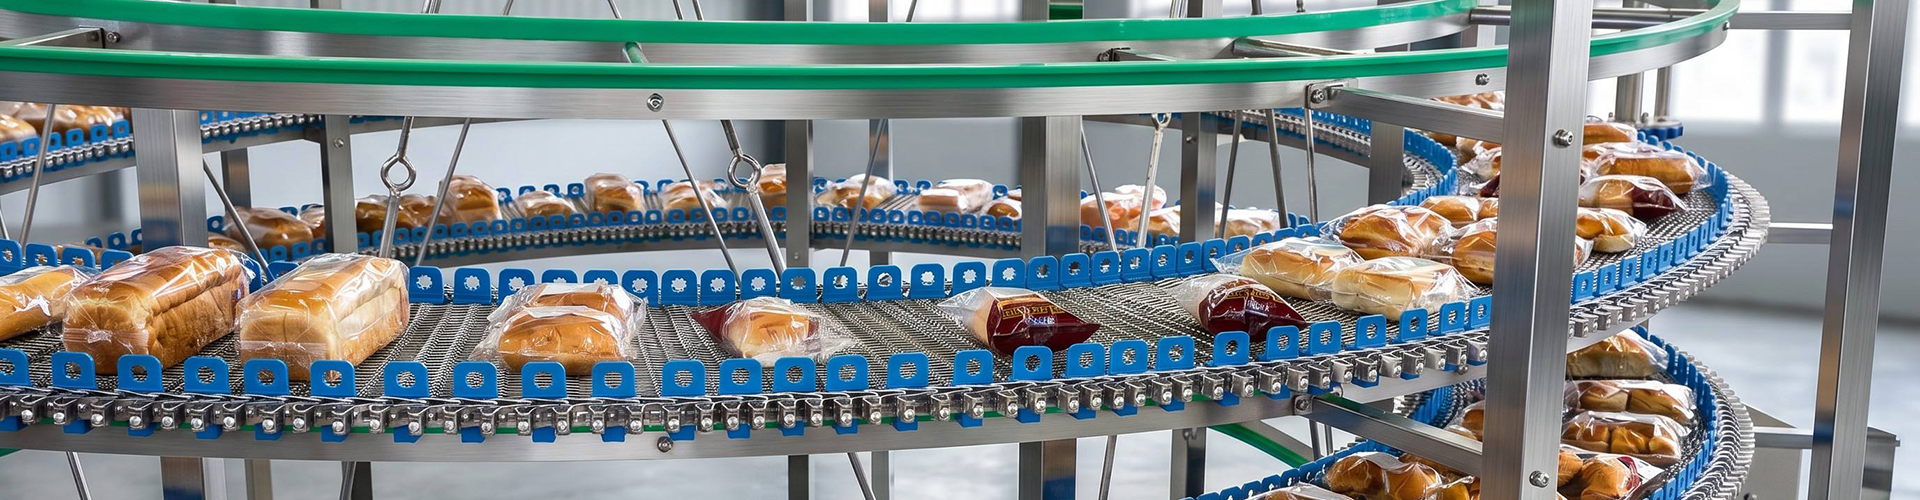


The Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing is a high-performance conveying solution designed for industries requiring hygienic, flexible, and efficient transportation. With advantages including durable stainless steel construction, excellent heat transfer capability, customizable mesh designs, and multifunctional applications, it provides reliable support for modern production systems.
By improving product handling efficiency, optimizing production layouts, and supporting automated operations, the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing helps businesses enhance productivity and maintain consistent product quality.
For companies seeking a durable, adaptable, and professional conveying solution, the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing delivers reliable performance across food processing, beverage, pharmaceutical, chemical, and industrial manufacturing applications.
The Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing is an advanced material handling solution designed to provide efficient, hygienic, and reliable transportation for modern production environments. Developed with high-quality stainless steel and durable mesh belt technology, this conveyor system is specially designed for industries that require continuous product movement, temperature control, and stable conveying performance.
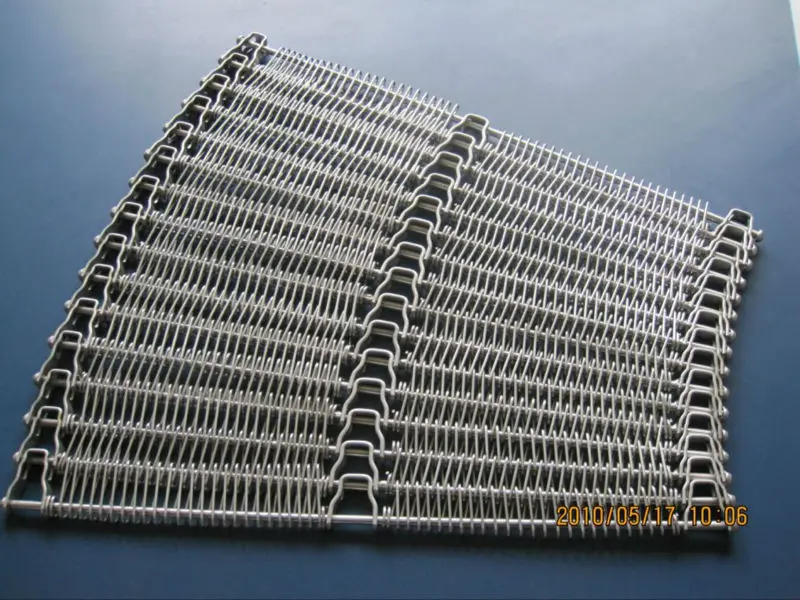
The Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing provides flexible transportation solutions for horizontal, inclined, and vertical conveying applications. Its mesh belt structure allows products to move smoothly through different production stages while maintaining excellent airflow, drainage, and heat transfer performance. This makes it especially suitable for food processing applications involving heating, baking, cooling, freezing, washing, and sterilization processes.
Designed for industrial flexibility, the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing can be customized with different mesh belt materials, widths, and structures according to specific product requirements. This allows manufacturers to achieve various conveying functions, including flat transportation, turning, lifting, lowering, and multi-level movement within a single production system.
The Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing is widely used in food production lines, packaging systems, and industrial automation processes. Its hygienic construction and reliable operation make it suitable for transporting food products, frozen seafood, beverage containers, electronic accessories, pharmaceutical products, and many other materials.
With its excellent adaptability and professional design, the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing helps businesses improve production efficiency, reduce manual handling, and create more organized automated workflows. It provides a practical solution for companies seeking a durable conveyor system capable of meeting different industrial transportation requirements.
Belt Material |
Carbon steel, stainless steel, thermoplastic chain |
|||
Frame Material |
Carbon steel, stainless steel |
|||
Strip Diameter(mm) |
1.2/1.6/2 or customized |
|||
Sprial Pitch |
12.7-40 or customized |
|||
Belt Width(mm) |
200-5000 or customized |
|||
Cross Rod Diameter(mm) |
3-8 or customized |
|||
Belt Length |
Customized |
|||
Upper/Lower Width(mm) |
Customized |
|||
Edge Finish |
Welded/Clenched |
|||
Sprockets |
Customized |
|||
The Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing offers outstanding advantages in performance, durability, and application flexibility. One of its most important features is its food-grade stainless steel construction, which provides excellent corrosion resistance, easy cleaning capability, and long-term durability. This makes the conveyor system ideal for industries where hygiene and product safety are critical.
A major advantage of the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing is its excellent airflow and heat transfer capability. The open mesh structure allows air, heat, and water to pass through easily, making it highly effective for baking, cooling, freezing, and drying processes. This helps improve product quality and ensures more consistent processing results.
The Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing provides highly flexible conveying options. Depending on production requirements, the conveyor can be configured for horizontal transportation, inclined movement, or vertical lifting. This flexibility allows manufacturers to optimize factory layouts and improve space utilization.
Another key feature of the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing is its ability to handle different product types. The mesh belt design can be customized according to product size, weight, and processing requirements. This allows the conveyor to transport delicate food products, frozen items, packaged goods, and industrial components safely and efficiently.
The Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing also offers strong adaptability through different belt materials and structural designs. Stainless steel mesh belts provide durability and hygienic performance, while other material options can meet different industrial conditions. This makes the equipment suitable for food processing, pharmaceutical production, chemical applications, and general manufacturing.
Operational stability is another important benefit of the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing. The reliable transmission structure ensures smooth product movement while reducing vibration and unnecessary interruptions. This helps maintain continuous production and improves overall manufacturing efficiency.
The conveyor system can also be developed into specialized industrial equipment by selecting suitable mesh belt designs. The Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing can be used as bottle coolers, elevators, bottle storage tables, vegetable cleaning systems, sterilization equipment, and meat transportation systems. This multifunctional capability provides additional value for businesses with diverse production needs.
Easy integration is another advantage of this conveyor solution. The Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing can be connected with existing production lines and automated equipment, helping manufacturers build complete material handling systems. Its customizable structure allows it to meet different factory layouts and production processes.
The Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing is widely used in food manufacturing industries due to its hygienic design and excellent processing adaptability. It is commonly applied in the transportation of baked goods, snacks, frozen aquatic products, vegetables, meat products, and other food materials during production.
In bakery production, the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing provides reliable transportation for heating and baking processes. The open mesh structure improves heat circulation and helps maintain consistent product quality during baking and cooling operations.
For frozen food and seafood processing industries, the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing offers efficient solutions for freezing transportation and cooling processes. Its corrosion-resistant construction allows stable operation in moisture-rich environments while maintaining hygienic production standards.
The beverage industry also benefits from the application of the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing. It can be used for transporting beverage bottles, aluminum cans, and packaged products through cooling, storage, and production lines. Its flexible design helps improve production organization and automation efficiency.
In pharmaceutical manufacturing, the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing provides a clean and reliable transportation platform for pharmaceutical products and packaging processes. The stainless steel structure supports strict hygiene requirements and stable product movement.
The daily chemical and cosmetics industries can also utilize this conveyor system for transporting bottles, containers, and packaged products. Its customizable mesh structure allows businesses to create efficient production lines according to different product characteristics.
Electronic accessory manufacturers can use the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing for transporting components and assembled products. The stable conveying performance supports automated production processes and improves workflow efficiency.
Beyond these applications, the Food Grade Stainless Steel Spiral Wire Mesh Conveyor Belt Conveyors for Food Processing can be integrated into specialized systems such as sterilizers, cleaning machines, cooling equipment, and lifting conveyors. Its versatility makes it a valuable solution for various industries requiring efficient and reliable material transportation.

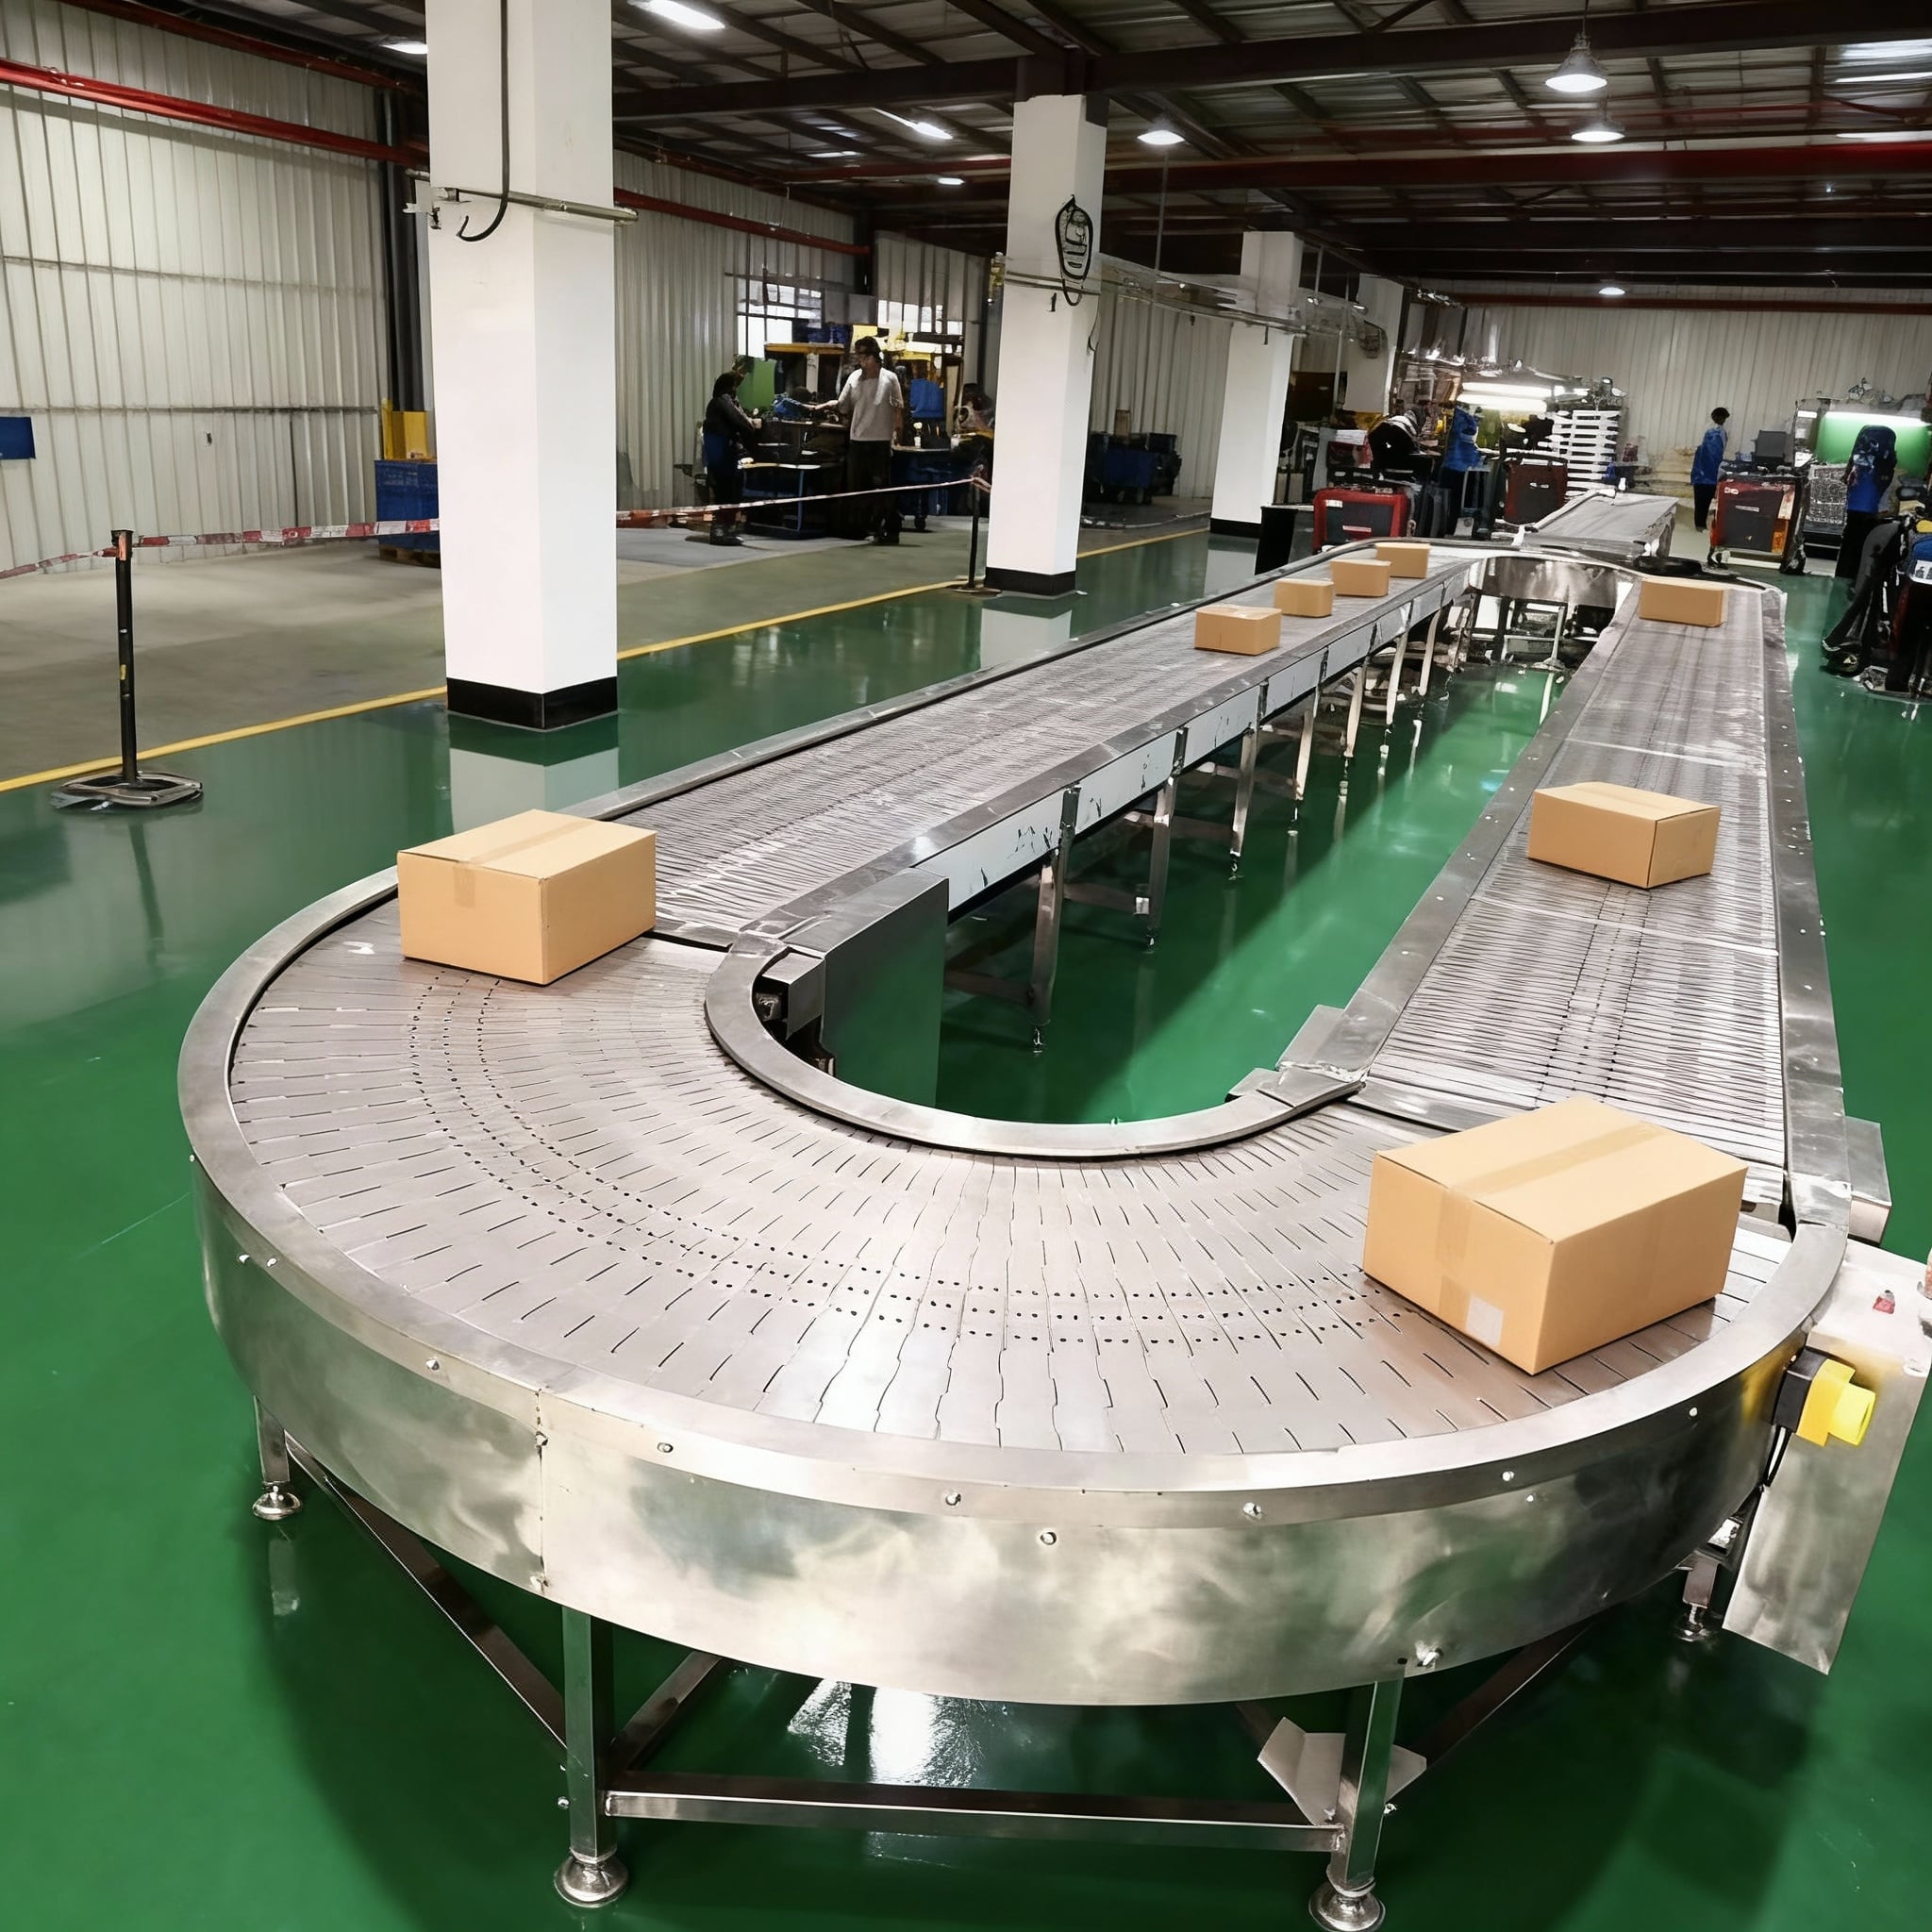
Circular Conveyor

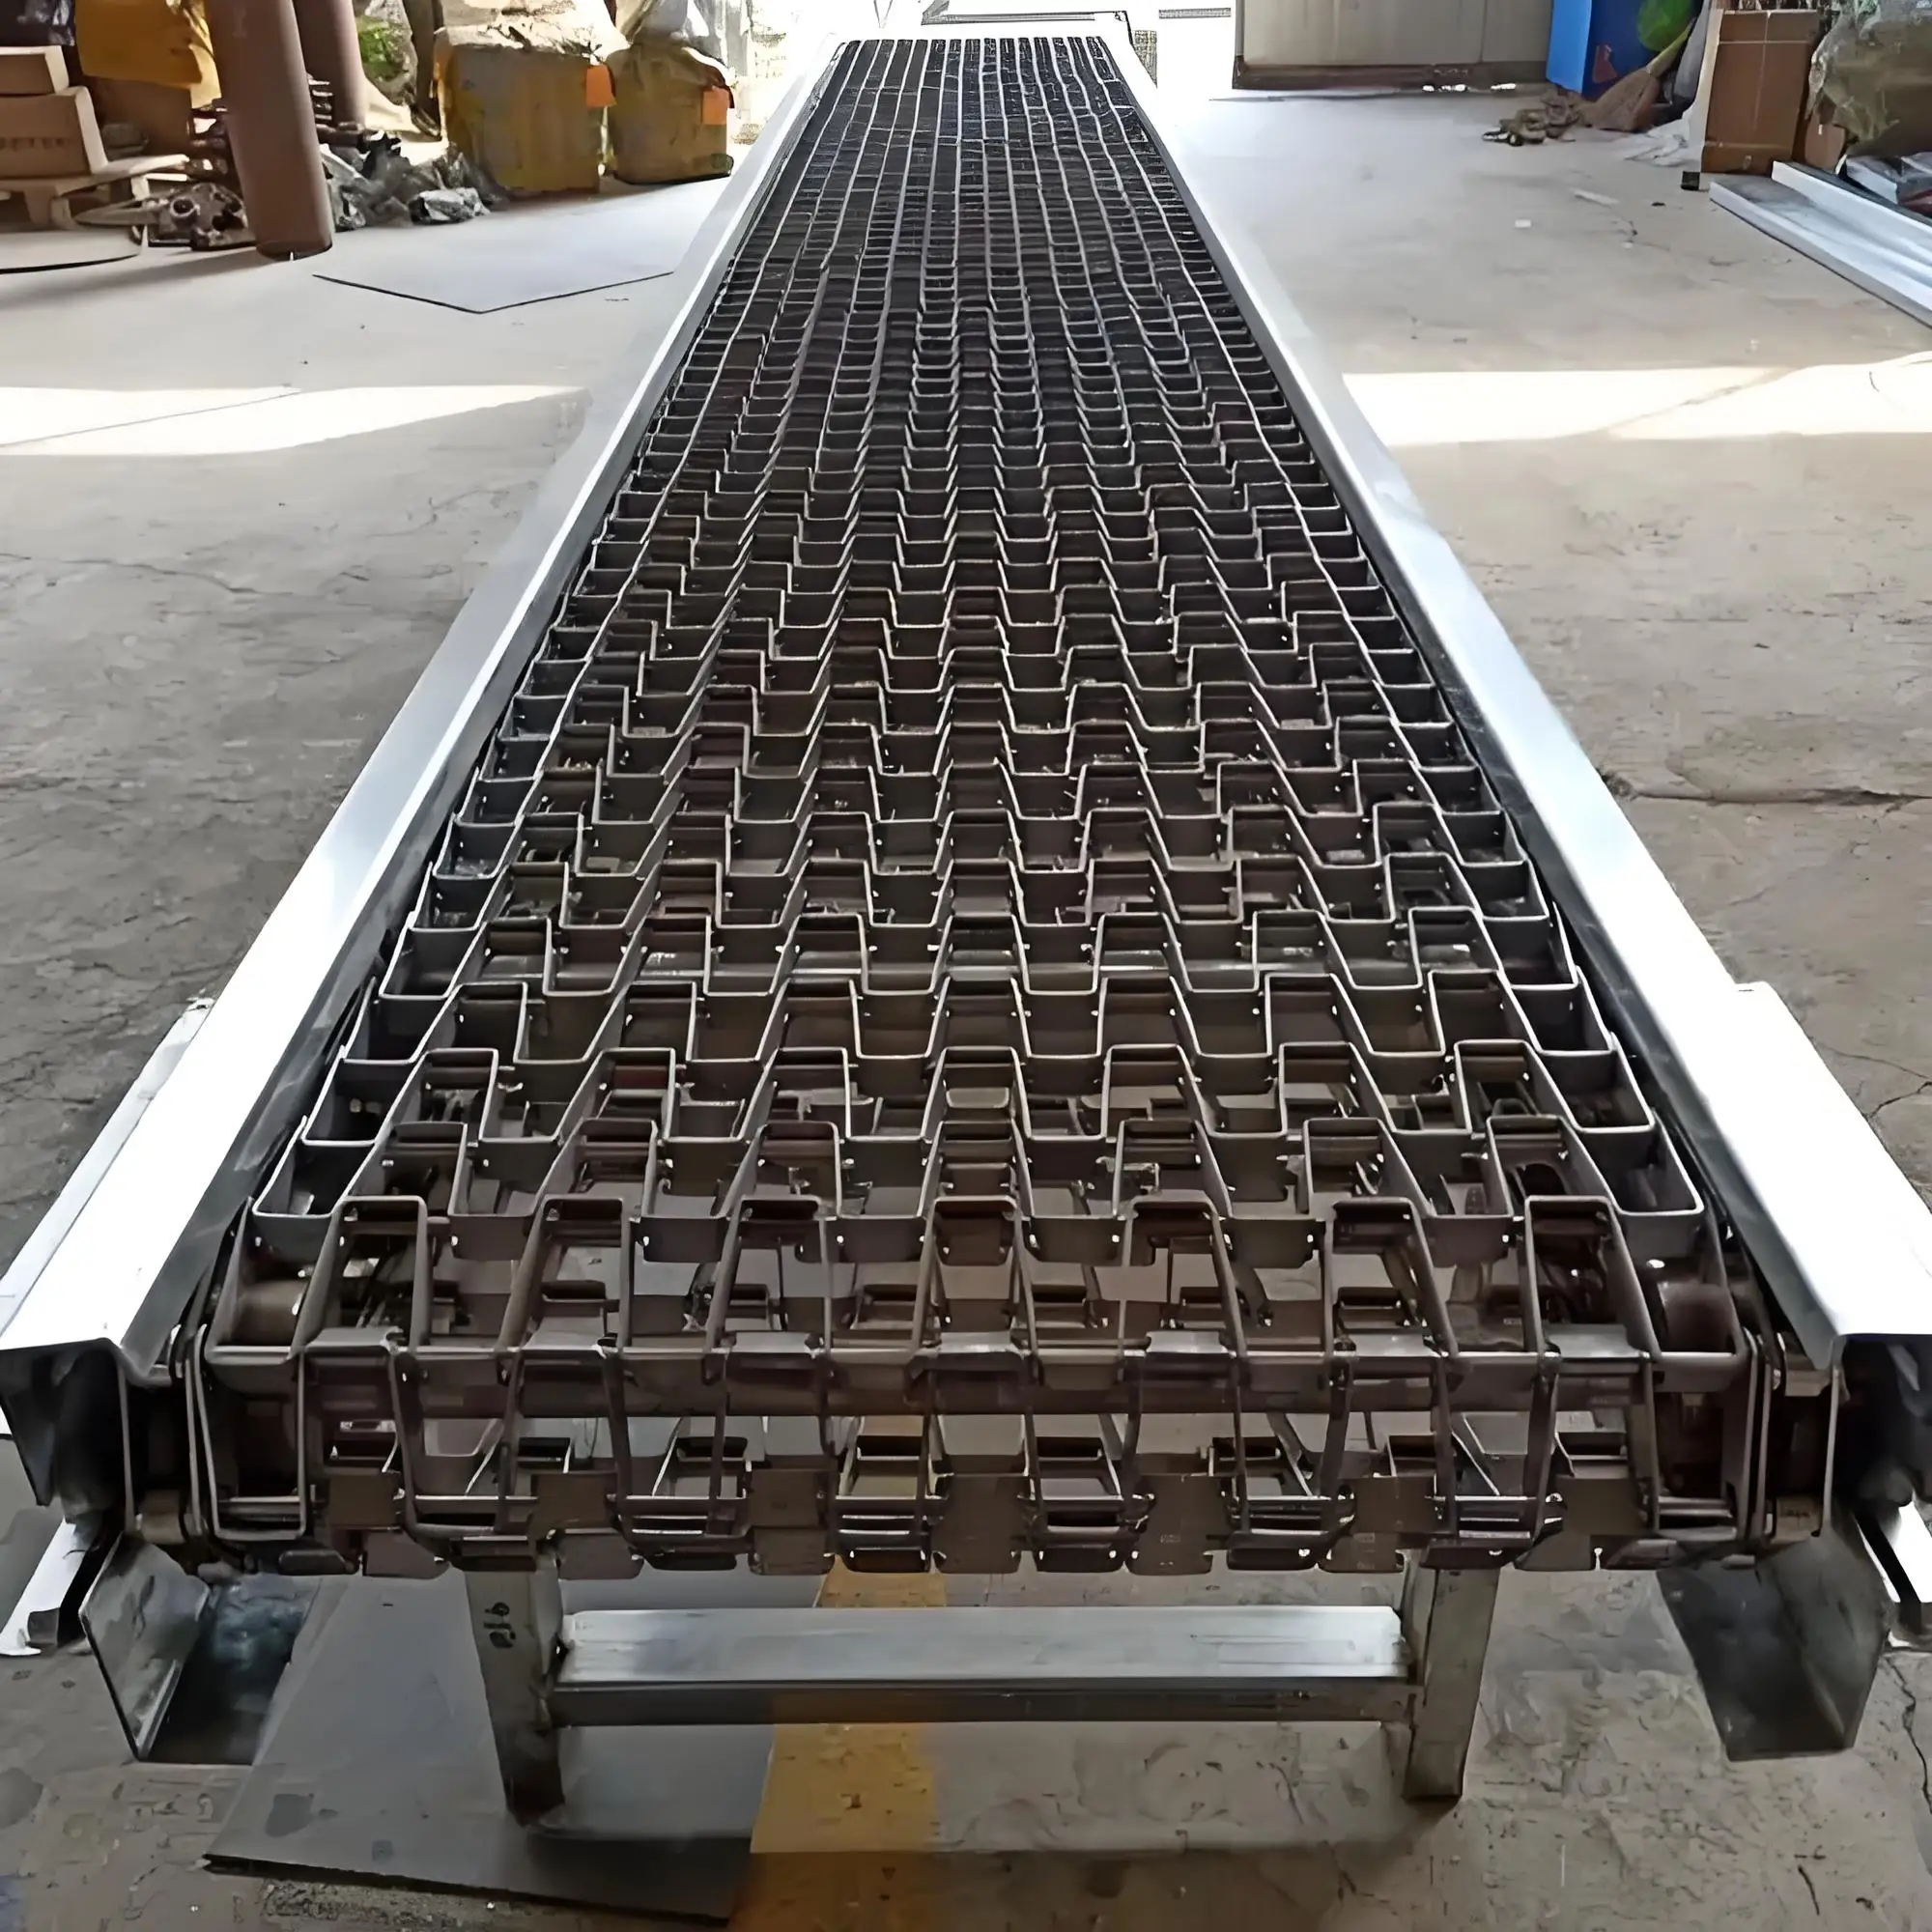
stainless steel wire mesh belt for transporting food use
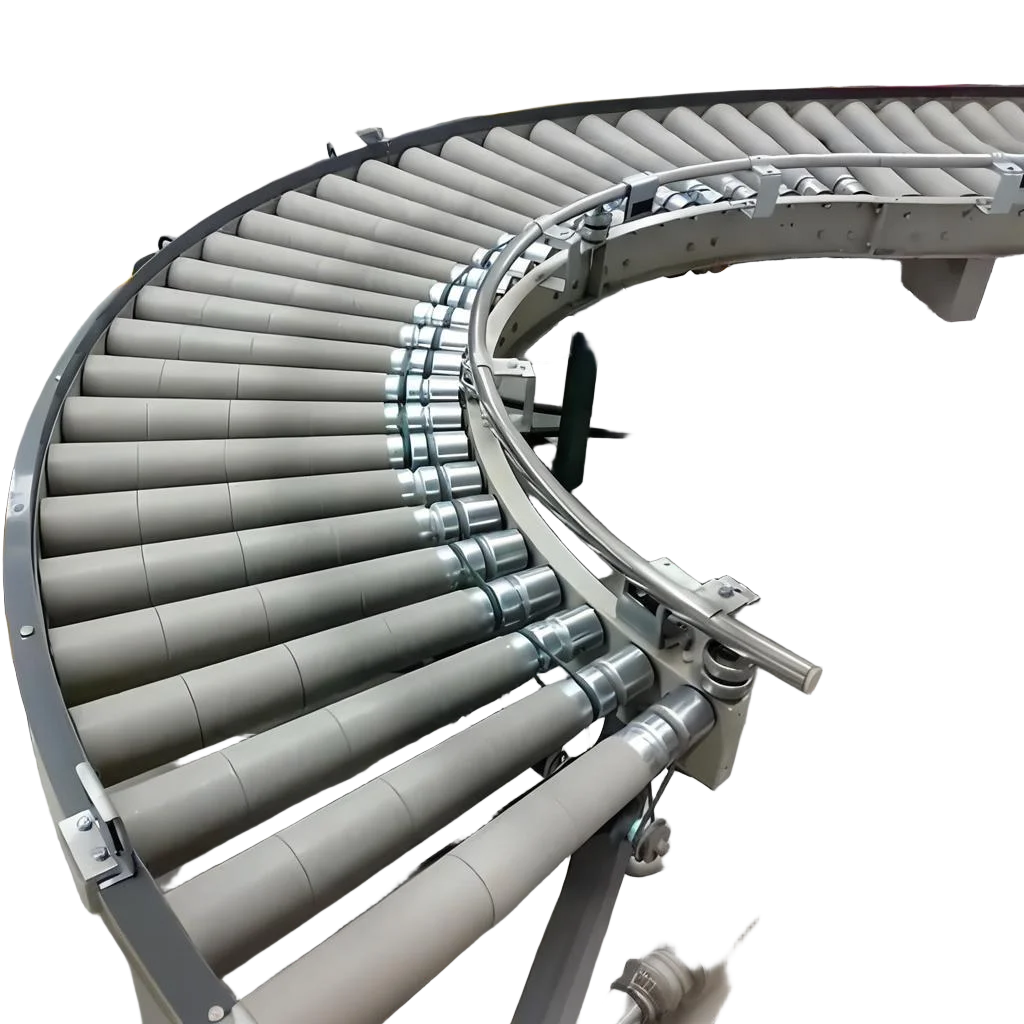
Heavy Duty Stainless Steel 90 Degree Outefeed Industrial Gravity Roller Conveyor Belt Roller Electric Conveyor

Industrial Endless Maize Water Jacketed Carbon Steel Screw Conveyor
Sunshine all products will make you absolutely satisfied, we always follow the customer first production concept, strive to open up domestic and foreign markets and are willing to establish long-term business cooperation with each customer. Welcome friends from all walks of life to come to guide, discuss cooperation!
 EN